HKXCAST一站式铝合金产品解决方案提供商邮箱:hkxcast@163.com
 10/24/2026
Sand casting vs die casting: tooling, piece price and the 2,000-10,000 part break-even, plus how tolerance and wall thickness shift the crossover.
 10/23/2026
Die casting machine tonnage sizing from 280T to 4000T. Learn the clamp force formula, projected area, safety factors, and how to match machine size to part.
 10/22/2026
Die casting intensification pressure packs metal against shrinkage in the third HPDC phase. Learn setting ranges, timing rules, and how to verify soundness.
 10/21/2026
Gate velocity in HPDC: why 30-60 m/s works, how to hit it with shot speed and gate size, and how shot curve monitoring keeps porosity down.
 10/20/2026
Die casting simulation shows fill pattern, air traps and porosity before tooling is cut. See which mold flow predictions to trust and which to verify by trial shot.
 10/19/2026
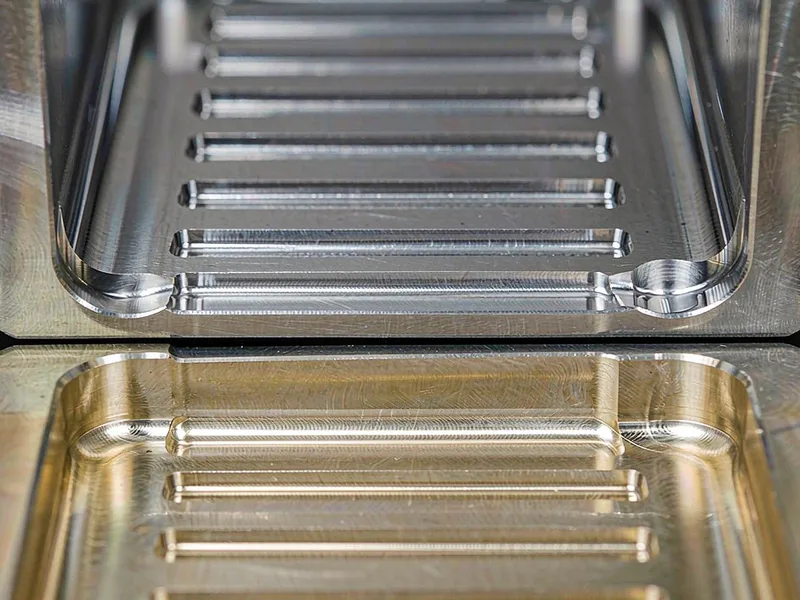
Die casting venting design guide: vent depth rules, overflow sizing, vacuum assist, and vent maintenance that keep porosity out of your castings.
 10/18/2026
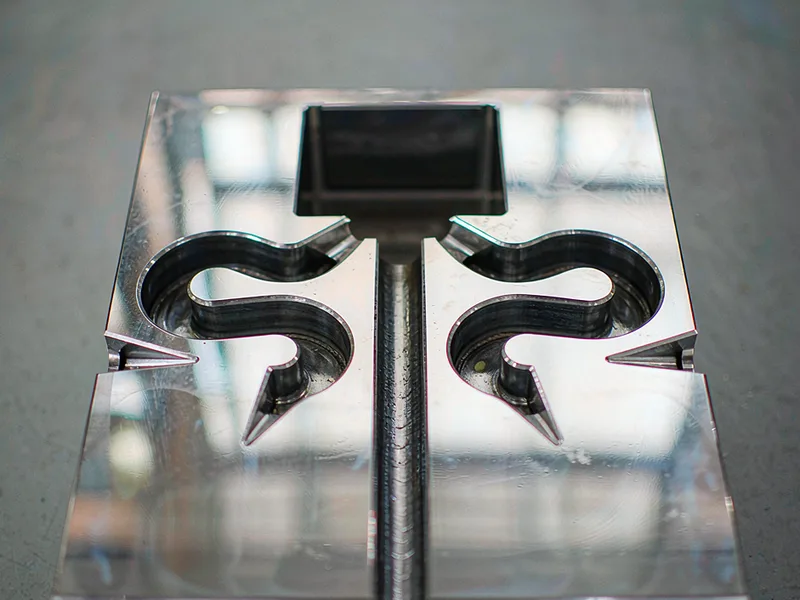
Die casting gating design guide: gate sizing, gate velocity, runner balancing, and fill patterns that stop cold shuts, jet flow, and porosity in HPDC.
 10/17/2026
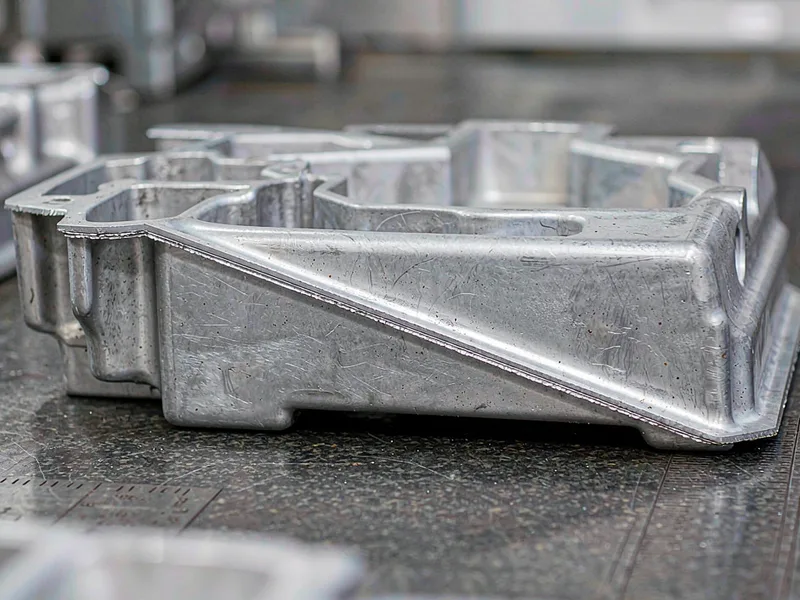
Die casting parting line design guide: where to split the mold, flat vs stepped lines, flash control, slide costs and tolerance rules that cut tooling cost.
 10/16/2026
Die casting draft angle guide: 1.5-2 degrees outside walls, 2-3 degrees on cores, plus texture, shrinkage and slide rules for cleaner release.
 10/15/2026
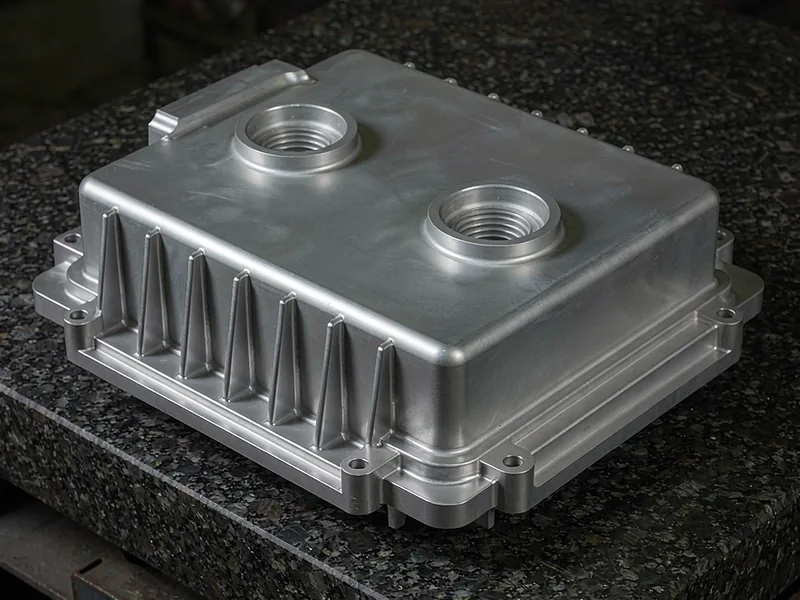
Minimum wall thickness for aluminum die casting: working numbers by alloy and size, design rules for ribs and bosses, and the real cost of going too thin.
 10/14/2026
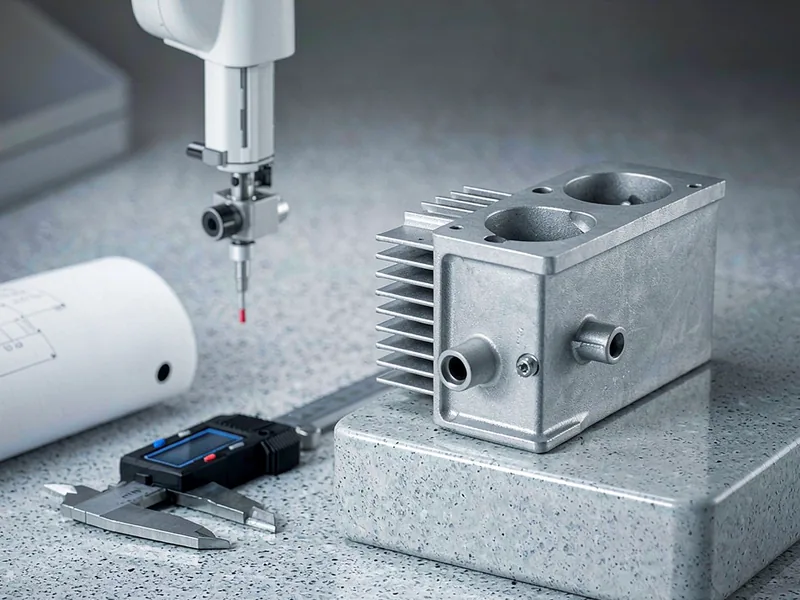
Die casting tolerances explained: NADCA Standard vs Precision limits, ISO 8062-3 CT grades, and how to spec tolerances that hold at volume.
 07/29/2026
China produces roughly 40% of the world’s aluminum castings, and US importers can typically save 30-50% on unit costs versus domestic suppliers — but only if they navigate HTS classification, Section 301 tariffs, and supplier vetting correctly. This 7-step guide on how to import aluminum casti…