Gate Velocity in HPDC: Working Inside the 30-60 m/s Window
Gate velocity is the single most sensitive number on a high pressure die casting shot. Set it too low and the metal freezes before the cavity fills. Set it too high and the front atomizes, dragging air into the casting. The working window for most aluminum die casting alloys sits between 30 and 60 m/s at the gate, and staying inside it separates a clean casting from a leak-test reject. This guide explains where the window comes from, how to hit it, and how to keep it under control on the floor.
Key Takeaways
- Target gate velocity for aluminum HPDC: 30–60 m/s, with 40–50 m/s as the comfort zone.
- Below about 25 m/s, fill is sluggish and cold shuts appear on thin sections.
- Above about 60 m/s, the metal front atomizes and entrains air, raising porosity.
- Gate speed comes from shot velocity, gate size, and metal pressure — you tune it with all three.
- Measure it with a shot curve and go/stop sensors, not by feel.
Why the 30-60 m/s Window Exists
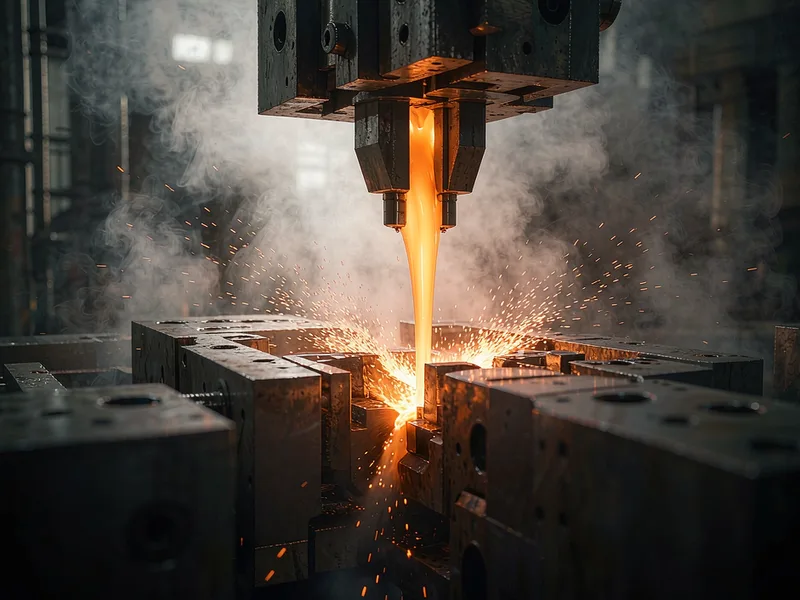
In HPDC, metal enters the cavity through a gate that is a fraction of a millimeter to a few millimeters thick. The plunger pushes at moderate speed, then the shot valve shifts and metal accelerates through that restriction. The gate velocity controls the shape of the metal front.
Under 30 m/s, the front stays coherent but slow. It loses heat to the die as it travels. Thin walls freeze before the front arrives, and you get weak seams and flow lines on the surface. The part may fill, but the seams show up in X-ray and fail under load.
Over 60 m/s, the front tears apart into droplets. Droplets fly ahead of the main front, trap air in pockets, and fold oxide skin back into the metal. That is the classic recipe for porosity and blistering. High speed also hammers the die surface near the gate, causing erosion and soldering that shorten tool life.
Inside the window, the front stays mostly coherent and still moves fast enough to beat freezing. That balance is why every gate design starts from this range and narrows it for the specific part.
Working Targets by Part and Alloy
The window shifts with alloy, wall thickness, and flow length. Use the table as a starting point, then tune on the machine with real shot traces.
| Condition | Alloy | Target speed at gate | Notes |
|---|---|---|---|
| General parts, 2–4 mm walls | A380 / ADC12 | 35–45 m/s | Default starting band for most work |
| Thin-wall electronics housings, ≤1.5 mm | ADC12 | 45–60 m/s | Speed fights short fill times |
| Thick structural parts, >5 mm | A360 / AlSi10Mg | 30–40 m/s | Lower speed, rely on intensification |
| Long flow path, >300 mm | A380 | 40–55 m/s | Extra speed covers heat loss |
| Cosmetic surfaces, no streaks | ADC12 | 40–50 m/s | Pair with good venting and overflows |
Numbers alone do not finish the job. Two castings with the same inlet speed can behave differently if venting, die temperature, or fill time differ. Treat the table as a launch point and verify each family with trial shots.
How Gate Speed Connects to the Shot Sleeve
Gate velocity is not a machine setting — it is a result. The shot tip velocity, the gate opening, and the metal pressure combine to set it, and the relation is simple: speed at the gate equals plunger velocity times the plunger area divided by the gate area.
That formula gives you two tuning knobs. Change the plunger speed in phase two, or change the gate opening in the die. Small gates raise velocity; wide gates lower it. A 10 percent change in gate size moves gate velocity by the same proportion, all else equal.
Metal pressure matters too. If the accumulator cannot deliver the pressure needed to push the chosen flow through the gate, the real velocity falls short of the setpoint. Check the P-Q² diagram before you promise a speed the machine cannot reach.
This is also where gate design happens. We size the gate from required fill time and cavity volume first, then check the resulting speed against the window, then adjust. Working backward from a velocity target alone ignores fill time, and working from fill time alone ignores the machine. Both must agree.
Measuring and Controlling Velocity in Production
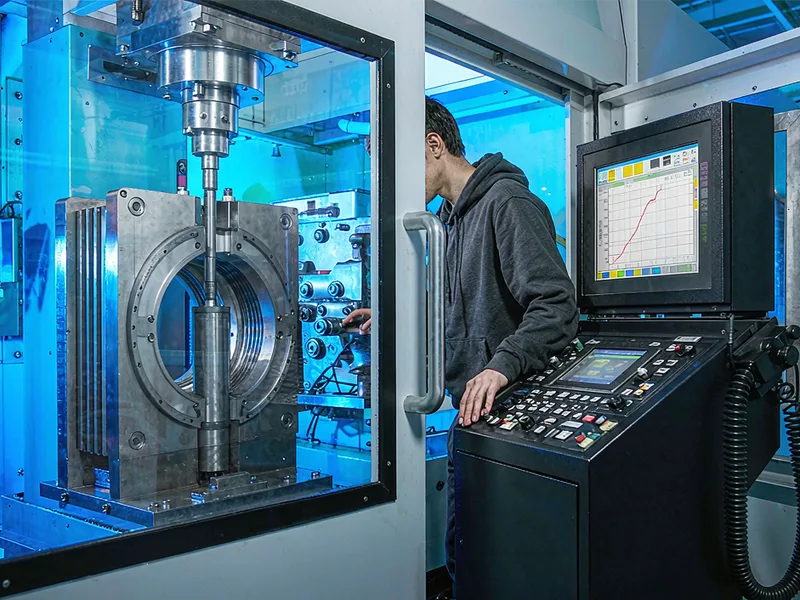
You cannot control what you cannot see. Modern shot ends carry shot curve monitoring: a position transducer on the plunger and pressure sensors on the accumulator and intensifier. Together they plot the real speed profile of every shot.
Read the curve in three zones. Zone one is slow sleeve fill, where the goal is a flat trace and no wave splash. Zone two is the fast stroke, where velocity climbs to setpoint. Zone three is intensification, where pressure spikes to pack the casting.
Set the changeover point with care. Too late, and metal freezes in the gate. Too early, and sleeve air enters the cavity. Go/stop sensors and real-time shot control hold the changeover point shot after shot, which is what keeps velocity stable.
Watch the spread, not just the average. A gate speed that wanders 5 m/s between shots will show up as scattered void results in X-ray. If the spread is wide, look for hydraulic drift, worn shot rings, or dirty sleeve lubrication before blaming the die.
Common Gate Speed Mistakes and How We Fix Them
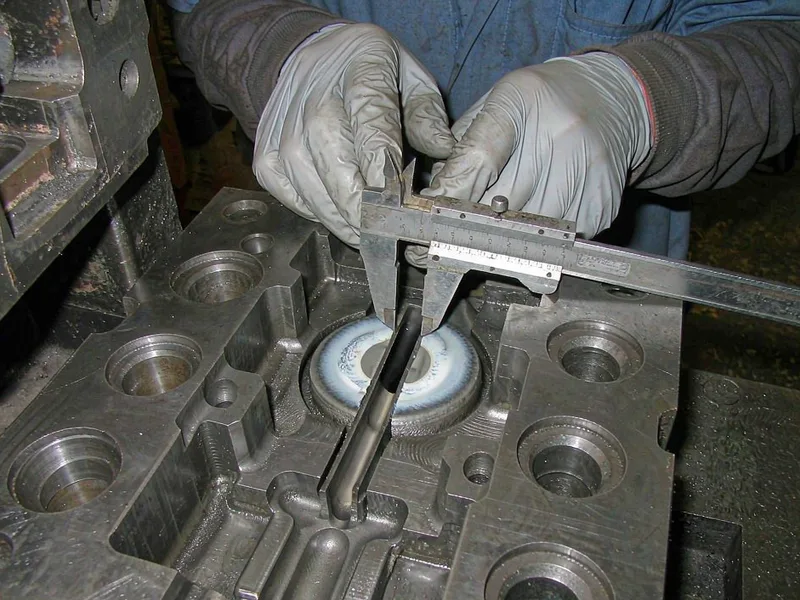
Mistake one: chasing speed to fix a cold shut. At 45 m/s the real cause is often a long flow path, a cold die, or poor venting. Raising speed past the window trades a surface defect for internal porosity. We fix the root cause first and keep speed in the band.
Mistake two: ignoring the sleeve phase. A rough first phase throws a wave down the sleeve and delivers a pre-contaminated shot to the gate. Slow the first phase, keep the wave flat, and the metal that reaches the gate is cleaner.
Mistake three: tuning without a curve. Guessing at velocities from sound or feel wastes shots and hides drift. We record the trace on every setup and compare it with the baseline from process sign-off. If the shape changes, the process has changed.
Mistake four: one velocity for every part in a die-cast family. Each cavity or part sees different flow resistance. Trim per-cavity gates so every branch lands inside the window, not just the average.
If you are fighting porosity or cold shuts and want a second opinion on your gate, send us the part print and your shot parameters. We will check the gate velocity, the gate size, and the fill time together, and tell you which knob actually needs turning.
External Links
- North American Die Casting Association (NADCA) — source of the widely used shot sleeve and gate design guidance referenced across the HPDC industry.
- ASM International — reference data on aluminum casting alloy behavior that supports fill and velocity decisions.
- ASTM B85 — standard specification for aluminum-alloy die castings, useful when tying process windows to alloy specs.
FAQ
What is the ideal gate velocity in HPDC?
For most aluminum parts, 40–50 m/s is the comfort zone. Thin walls run closer to 60 m/s, thick structural parts closer to 30–40 m/s. The right value balances fill time against air entrapment for your specific part.
What happens if gate speed is too high?
Above roughly 60 m/s the metal front atomizes, entrains air, and folds oxide into the casting. Porosity, blisters, and gate erosion rise sharply. Parts may also show smoke stains near the gate.
What happens if gate speed is too low?
Below about 30 m/s the front moves too slowly to beat freezing. Weak seams, flow lines, and incomplete fill appear on thin sections. The fix is usually more speed or a shorter, hotter flow path.
How do you calculate die casting gate velocity?
Gate speed equals plunger velocity multiplied by plunger area, divided by gate area. Measure the real plunger speed from the trace, since hydraulic losses make setpoint and actual differ.
Does gate speed affect porosity?
Yes, strongly. Excess velocity atomizes the front and traps air; too little velocity creates cold shuts that act like internal defects. Keeping speed inside the window, with good venting and a clean sleeve phase, is the main defense against gas porosity.